+86 0512 68562392
Contact Us
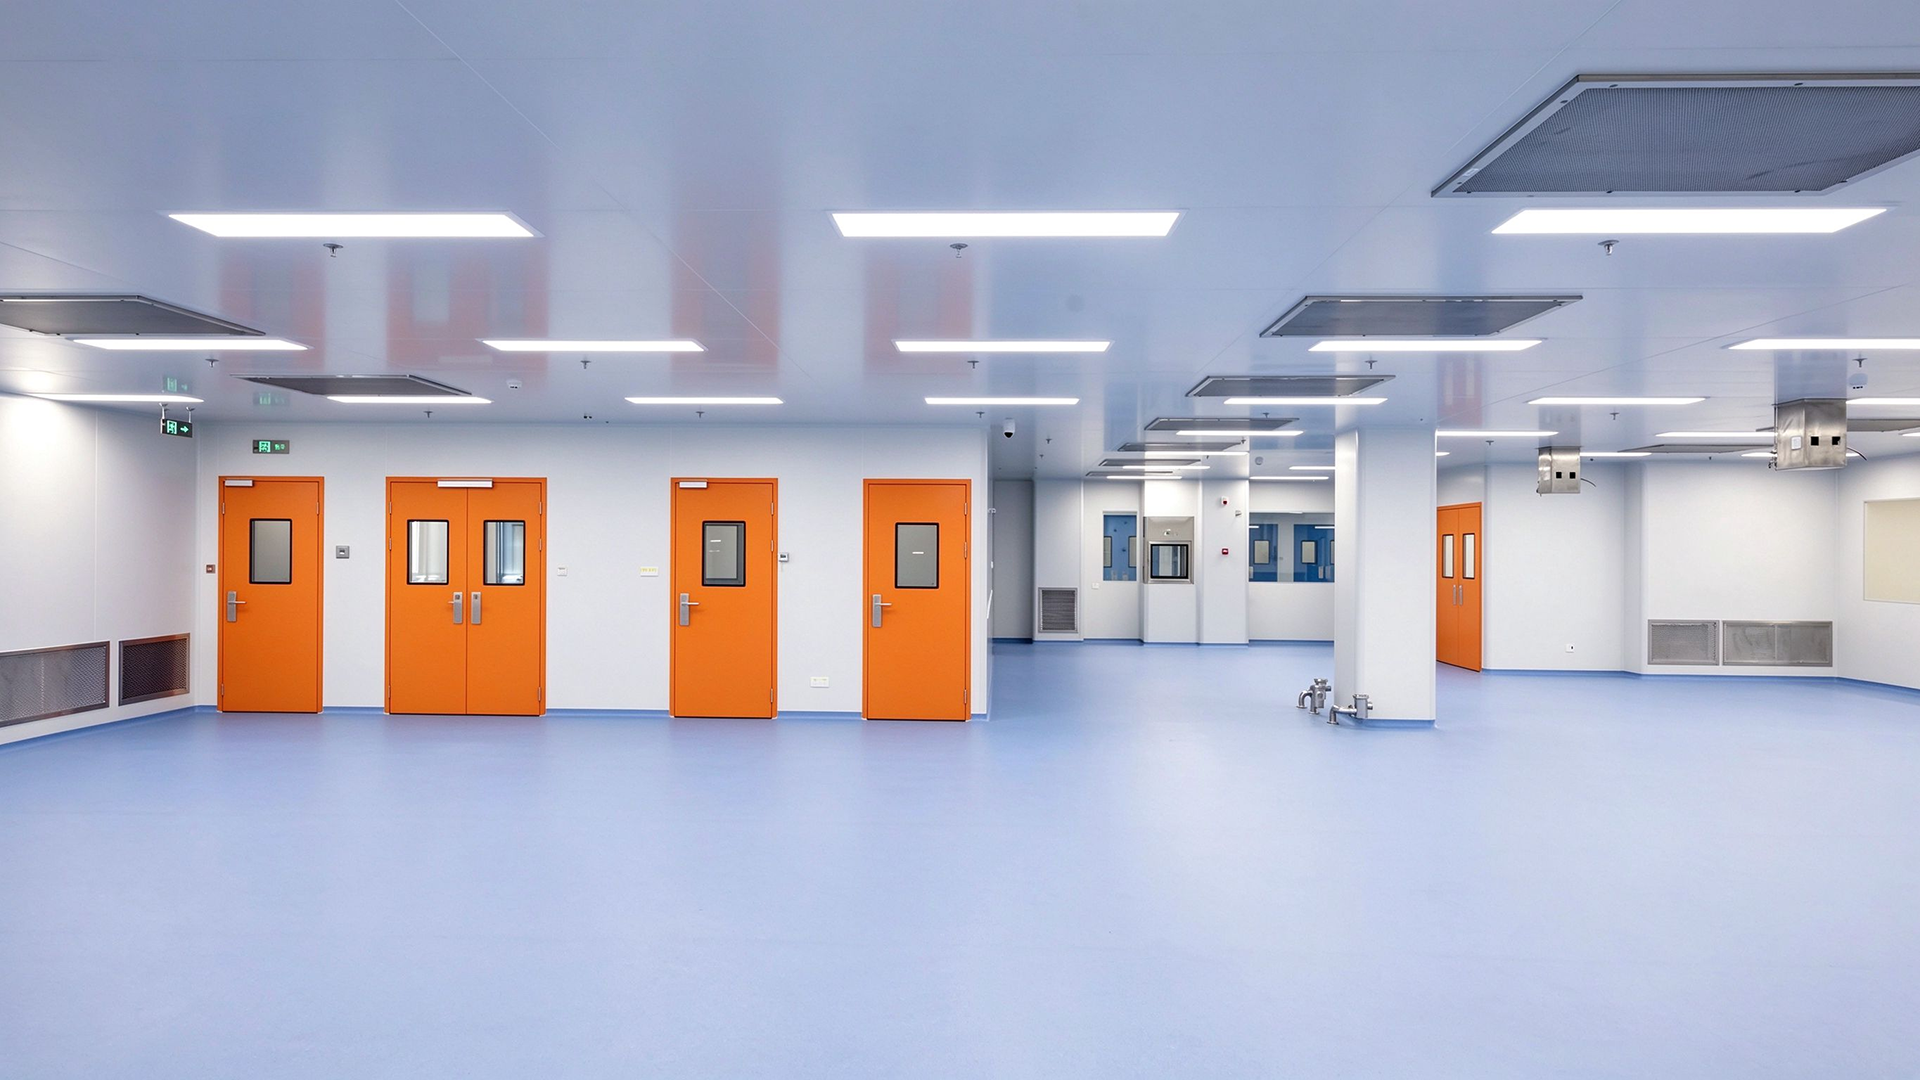
At EasyCube, we deliver tailored, high-integrity controlled environments engineered specifically for the evolving demands of food, beverage, and nutraceutical processing. Our patented prefabricated system bypasses the friction of traditional on-site construction, allowing food products to deploy scalable hygienic production lines with unmatched speed and structural predictability.
Our solutions are engineered to meet the world’s most rigorous quality and safety benchmarks, ensuring your facility is audit-ready from day one:
Standards: ISO 14644 (Class 1–100,000)
Regulatory Alignment: FDA (US), cGMP (21 CFR Part 110/117), HACCP, and international SQF/BRCGS guidelines
Our modular solutions are engineered to support the entire lifecycle of food and nutrition development, providing specialized environments from ingredient processing to clean filling, from R&D to pilot scale to full commercial production. We provide precisely controlled spaces for a comprehensive range of food and nutrition applications, such as:
Certified environments optimized for blending, tableting, encapsulation, and packaging of vitamins and botanicals.
Positive pressure zones designed to prevent Cronobacter, Salmonella, and other microbial risks during critical handling.
Specialized containment suites for the synthesis, harvesting, and processing of high-value bio-ingredients, enzymes, and oligosaccharides.
Ultra-sterile Class 100 (ISO 5) environments for sterile filling and final packaging to extend shelf life naturally.
Precise climate and humidity-controlled environments engineered to manage moisture-sensitive ingredients and eliminate cross-batch contamination.